전체 방송국 검색
Lyophilization sits at the core of modern drug manufacturing. Vaccines, biologics, monoclonal antibodies, and a growing share of injectable therapeutics simply cannot survive in liquid form long enough to be shipped, stored, and administered reliably. A properly specified pharmaceutical freeze dryer is what makes these products viable at all — turning an unstable liquid formulation into a stable, long-shelf-life product that can travel across the world and sit on a shelf for years without losing potency.
Many of the most important therapeutics developed in the last two decades — vaccines, protein-based biologics, peptides, and monoclonal antibodies — are inherently unstable in aqueous solution. Left in liquid form, these molecules degrade, aggregate, or lose potency well before they can reach a patient. Traditional heat-based drying destroys the same delicate molecular structures these drugs depend on to function.
Freeze drying of pharmaceutical products solves this by removing water through sublimation at low temperature, avoiding the thermal stress that would otherwise denature proteins or degrade active compounds. The result is a stable, dry cake or powder that can be reconstituted with a diluent immediately before use, restoring the product close to its original potency and structure.
This is why a freeze dryer pharmaceutical application looks fundamentally different from freeze drying used in food processing or general laboratory work. Pharmaceutical lyophilization must meet strict regulatory requirements around sterility, batch consistency, process validation, and documentation — every cycle needs to be reproducible down to fractions of a degree and every batch needs a complete data trail for regulatory submission.
The lyophilization cycle used across the freeze dryer pharmaceutical industry follows three carefully controlled phases:
Freezing: The formulation, typically already filled into vials on the freeze dryer’s shelves, is frozen to a temperature well below its eutectic or glass transition point — often between -40°C and -50°C. Getting this step right is critical; incomplete freezing at this stage can cause structural collapse later in the cycle.
Primary Drying (Sublimation): Once fully frozen, the chamber pressure is reduced dramatically under vacuum, and shelf temperature is raised slightly in a tightly controlled ramp. This causes the frozen water to sublimate directly into vapor without melting, which is then captured on a refrigerated condenser. This phase typically accounts for the majority of total cycle time — often 20 to 40+ hours for complex biologic formulations.
Secondary Drying: After the bulk of the ice has sublimated, shelf temperature is raised further to remove any remaining bound moisture that wasn’t released during primary drying. This step is essential for achieving the low residual moisture levels required for long-term pharmaceutical stability, typically well under 1-2%.
Throughout the entire cycle, a pharmaceutical freeze dryer used in a regulated production environment logs shelf temperature, chamber pressure, and condenser performance continuously, generating the documentation required for batch release and regulatory compliance.
One of the most consequential decisions in specifying lyophilization equipment is sizing the system correctly for current and future production needs. The gap between a medium pharmaceutical freeze dryer and a large pharmaceutical freeze dryer isn’t just about chamber size — it affects capital cost, facility requirements, validation complexity, and long-term production flexibility.
A medium pharmaceutical freeze dryer typically serves clinical trial manufacturing, pilot-scale production, and mid-volume commercial batches. These systems offer enough shelf area and condenser capacity to process meaningful batch sizes — often several thousand vials per cycle — while remaining manageable in terms of facility footprint, utility requirements, and capital investment.
This size class is particularly common among contract development and manufacturing organizations (CDMOs), specialty biotech companies producing lower-volume therapeutics, and manufacturers scaling up from lab-scale development toward commercial production. A mid-size system also offers a practical entry point for companies validating a new formulation before committing to full industrial-scale infrastructure.
A large pharmaceutical freeze dryer is built for high-volume commercial manufacturing, where thousands to tens of thousands of vials must be processed per cycle to meet market demand. These systems require significantly more shelf area, larger condensers capable of capturing correspondingly higher moisture loads, and heavier-duty vacuum systems to maintain uniform pressure across a much larger chamber.
Facilities running a large pharmaceutical freeze dryer typically integrate the unit directly with automated loading and unloading systems, isolator or RABS (restricted access barrier system) technology for aseptic processing, and full automation of the stoppering process to maintain sterility at scale. This level of system is common among large pharmaceutical manufacturers producing vaccines, widely prescribed biologics, and other high-volume injectable products.
The right choice between a medium and large system comes down to a few key factors:
Many manufacturers ultimately operate both — a medium system for clinical supply, formulation development, and smaller product lines, alongside a large system dedicated to established, high-volume commercial products.
Whether evaluating a medium pharmaceutical freeze dryer or scaling up to a large pharmaceutical freeze dryer, several specifications determine whether a system will actually meet GMP production and regulatory requirements.
Consistent shelf temperature across the entire chamber is essential for producing uniform product from vial to vial, regardless of position on the shelf. Poor temperature uniformity leads to batch variability, with some vials fully dried while others retain excess moisture — a serious quality and regulatory concern. Look for systems with tight temperature uniformity specifications and validated mapping data across the full shelf area.
Condenser performance directly affects both cycle time and the maximum batch size a system can process without risking vapor breakthrough. Pharmaceutical-grade systems typically require condenser temperatures in the -60°C to -85°C range, with total ice capacity scaled appropriately to the shelf area and expected moisture load of a full batch.
For any system operating at commercial scale, automated loading and stoppering capability is essential — not just for efficiency, but for maintaining sterility throughout the process. Vials must be automatically seated with their stoppers under vacuum at the end of the cycle, before the chamber is brought back to atmospheric pressure, to prevent microbial ingress during unloading.
Pharmaceutical production environments require rigorous cleaning and sterilization validation between batches, particularly for products manufactured under aseptic conditions. Systems with integrated CIP and SIP capability significantly reduce changeover time and support the documentation requirements auditors expect during regulatory inspections.
Regulatory bodies require complete, tamper-evident documentation of every production cycle, including shelf temperature, chamber pressure, and timing data throughout freezing, primary drying, and secondary drying. A pharmaceutical freeze dryer intended for regulated manufacturing should offer 21 CFR Part 11-compliant data logging, electronic batch records, and audit trail functionality integrated directly into the control system.
For aseptic processing of sterile injectables, integration with isolator or RABS technology maintains a controlled barrier between operators and the product throughout loading, processing, and unloading. This is increasingly a standard expectation for both medium and large-scale systems producing sterile injectable products.
Given the long cycle times typical of pharmaceutical lyophilization — often 40 hours or more for complex biologics — energy consumption becomes a meaningful operating cost over the equipment’s lifetime. Facilities should evaluate refrigeration system efficiency, vacuum pump power draw, and heat recovery options when comparing systems, particularly for a large pharmaceutical freeze dryer running near-continuous production cycles.
Many vaccines, particularly those based on live attenuated viruses or mRNA technology, require lyophilization to remain stable outside of ultra-cold storage. A pharmaceutical freeze dryer capable of precise, validated cycle control is essential to producing vaccine batches that meet both potency and stability requirements across global distribution and storage conditions.
Protein-based therapeutics are highly sensitive to degradation in liquid form. Freeze drying of pharmaceutical products in this category extends shelf life dramatically, allows for room-temperature or refrigerated storage instead of frozen distribution, and simplifies the cold chain logistics that would otherwise be required for a liquid biologic product.
A wide range of injectable small-molecule drugs are formulated as lyophilized powders for reconstitution, particularly when the active compound is unstable in aqueous solution over extended storage periods. This remains one of the most common and well-established uses across the freeze dryer pharmaceutical industry.
Beyond therapeutics, pharmaceutical-grade freeze drying is used extensively to stabilize diagnostic reagents, enzymes, and other components used in point-of-care testing kits, extending shelf life and removing the need for cold-chain shipping for many diagnostic products.
Companies advancing a new formulation through clinical development often rely on a medium pharmaceutical freeze dryer to produce the smaller batch sizes required for Phase I through Phase III trials, before scaling to commercial production volumes on a larger system once the product reaches market approval.
Any facility installing a freeze dryer pharmaceutical system for commercial or clinical production must account for the regulatory framework governing sterile drug manufacturing. This typically includes:
Equipment vendors serving the pharmaceutical industry typically provide qualification support and documentation packages specifically designed to streamline this validation process, which is worth factoring into vendor selection alongside the equipment’s core technical specifications.
Cake Collapse and Structural Defects: Poor shelf temperature control or inadequate vacuum performance can cause the frozen cake to collapse during primary drying, resulting in a compromised final product. Systems with tight temperature uniformity and reliable, well-mapped shelf performance significantly reduce this risk.
Inconsistent Residual Moisture: Variability in vial position, shelf temperature, or vacuum distribution can lead to inconsistent residual moisture across a batch, directly affecting product stability and shelf life. Reliable, validated equipment with strong temperature and pressure uniformity minimizes batch-to-batch and vial-to-vial variability.
Long Cycle Times Limiting Throughput: Complex biologic formulations often require extended primary and secondary drying phases to avoid product damage. A well-specified large pharmaceutical freeze dryer with strong condenser and vacuum performance can meaningfully reduce cycle time without compromising product quality, directly improving facility throughput.
Scale-Up Failures: A formulation developed and validated on lab-scale or medium-scale equipment doesn’t always transfer cleanly to larger systems, since shelf geometry, vacuum dynamics, and thermal behavior change with scale. Working with equipment manufacturers experienced in scale-up from medium pharmaceutical freeze dryer systems to full commercial large pharmaceutical freeze dryer installations helps reduce the risk of costly reformulation or re-validation later in development.ckages specifically designed to streamline this validation process, which is worth factoring into vendor selection alongside the equipment’s core technical specifications.
Selecting equipment for freeze drying of pharmaceutical products is as much about the manufacturer’s experience and support infrastructure as it is about the equipment specifications themselves. Look for a vendor with a demonstrated track record supplying the freeze dryer pharmaceutical industry, including:
A pharmaceutical freeze dryer is a long-term capital investment that will directly shape production capacity, product quality, and regulatory compliance for years. Choosing equipment sized correctly for current needs — while leaving a clear path to scale from a medium pharmaceutical freeze dryer toward a large pharmaceutical freeze dryer as production volume grows — gives manufacturers the flexibility to expand without costly reformulation or re-validation down the line.
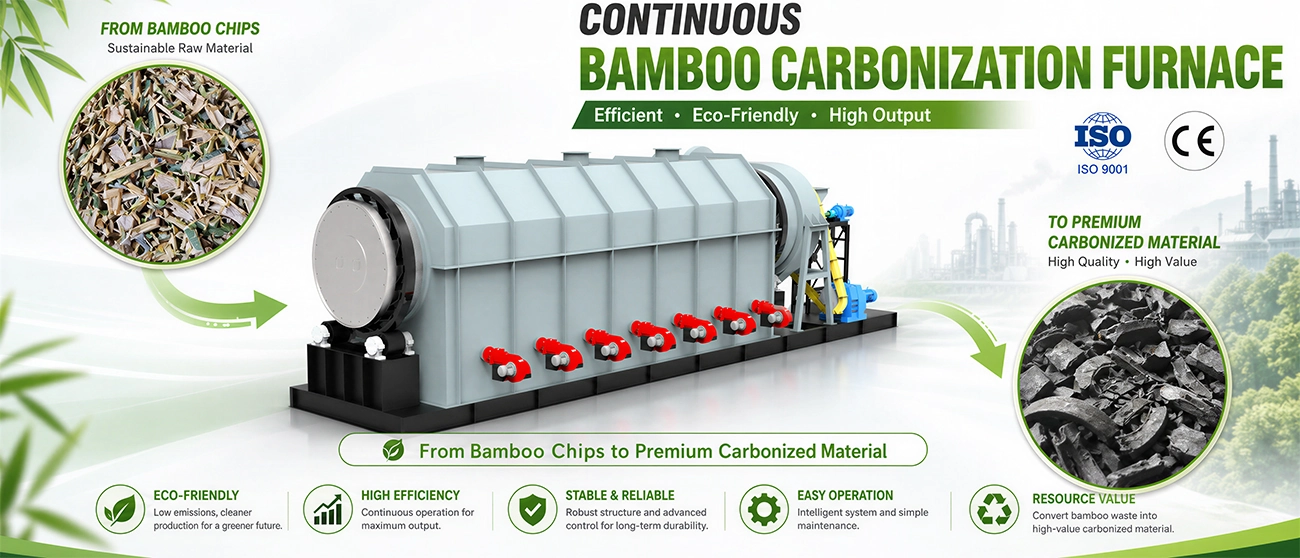
| Model | XY-800 | XY-1000 | XY-1200 | XY-1500 | XY-1800 | XY-2000 |
| Number of cylinder layers | Single | Single | Double | Double | Double | Double |
| Cylinder diameter | 800mm | 1000mm | 1200/700mm | 1500/900mm | 1800/1200mm | 2000/1500mm |
| Capacity | 200-300kg/h | 300-400kg/h | 450-600kg/h | 600-800kg/h | 800-1000kg/h | 1000-1200kg/h |
| Cylinder material | 309S/310S/316L | 309S/310S/316L | 309S/310S/316L | 309S/310S/316L | 309S/310S/316L | 309S/310S/316L |
| Temerature | 500-800ºC | 500-800ºC | 500-800ºC | 500-800ºC | 500-800ºC | 500-800ºC |
| Carbonization time | 20-60min | 20-60min | 20-60min | 20-60min | 20-60min | 20-60min |
| Raw material particle size | ≤4cm | ≤4cm | ≤4cm | ≤4cm | ≤4cm | ≤4cm |
| Heating method | indirect heating | indirect heating | indirect heating | indirect heating | indirect heating | indirect heating |
| Operation mode | continuously working | continuously working | continuously working | continuously working | continuously working | continuously working |
| Control method | PLC control | PLC control | PLC control | PLC control | PLC control | PLC control |
Frequently asked questions
A stainless steel reactor relies on the corrosion resistance of the alloy itself, which can degrade over time when exposed to strong acids, chlorides, or oxidizing agents. A glass lined reactor uses a fused glass barrier that offers superior resistance to a much broader range of aggressive chemicals, though it requires more careful handling to avoid mechanical damage to the lining.
With proper installation, operation, and maintenance, a glass lined reactor can provide more than 10 years of reliable service. Lifespan depends on process conditions, thermal cycling practices, and how well the lining is protected from mechanical impact.
Yes, many glass reactor vessel configurations are rated for vacuum operation, making them suitable for solvent recovery, vacuum distillation, and degassing applications. Vacuum-rated units require appropriate glass wall thickness and properly sealed ground-glass joints.
Choose a glass reactor when visual process monitoring, broad chemical compatibility, and modular reconfiguration matter most — typically at bench to kilo-lab scale. Choose a stainless steel reactor when you need higher pressure ratings, larger production-scale capacity, or greater mechanical durability for a validated, high-volume process.
Yes, we can supply complete jacketed glass reactor packages bundled with a compatible heating/cooling circulator sized to your required temperature range, or advise on circulator selection if you’re sourcing one separately.
 xuye